If you’re a Packaging Engineer or Production Manager staring down a wall of weekly order sheets that read “+15% volume this quarter” and wondering if your VFFS setup is keeping up, you’ve probably asked this exact question: single-lane vs multi-lane VFFS machines— which one’s actually built for high-volume production? I’m Alex, and I’ve spent the last 10 years selling and troubleshooting VFFS machines for a living, so let’s skip the jargon-heavy sales fluff and cut to the real, on-the-floor stuff no one tells you about. Vertical Form Fill Seal Machine(VFFS)
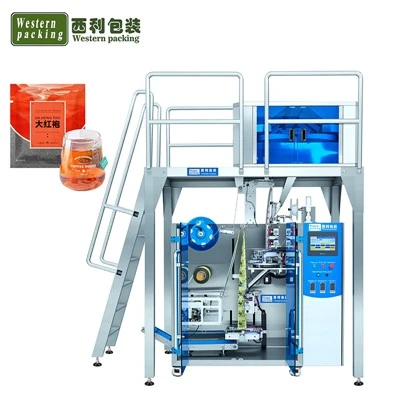
First, let’s define what we’re even talking about, because I’ve had so many clients come in mixing these up like they’re interchangeable socks. A single-lane VFFS is basically one production line in a single frame: it forms one pouch, fills it, seals it, cuts it, and sends it on its way. A multi-lane? Think 2, 4, even 6 lanes all running at the same time, side-by-side, inside one big machine body. Same core steps, just more copies of each lane crammed into the same footprint.
When I talk to clients chasing high-volume production—think 50k+ pouches a week, and growing fast—everyone’s first thought is “more lanes = more output, so multi-lane is the no-brainer.” But here’s the mistake I see 9 out of 10 new owners make: they buy a 6-lane machine for a 40k pouch weekly order, then realize they’ve traded one set of problems for a whole new bag of headaches that eat into actual uptime. Let’s break this down with real examples, no hypothetical numbers.
Take a snack food client I worked with last year. They were rolling out a small granola bar pouch that was flying off shelves, and their old single-lane was maxing out at 12k pouches a week. Their operations lead came to me screaming about missed deadlines, so I showed them a 4-lane multi-lane machine. At first, it looked perfect: 4 lanes running at 60 pouches per minute each meant 240 pouches per minute, 14,400 per hour, way more than they needed. But three months later, they called me in panicking. Why? Because that multi-lane machine isn’t just running 4 lanes—it’s got 4 sets of everything: 4 filling nozzles, 4 sealing jaws, 4 cutters. If one lane jams? The entire line stops. And fixing that jam takes 10 to 15 minutes of shutting down the whole machine, not just one side. Their uptime dropped from 92% with the single-lane to 78% with the multi-lane, and they were actually producing fewer usable pouches total than they were with the old setup.
Single-lane machines, on the other hand, might look slow on paper—they top out around 60 to 80 pouches per minute, max—but their uptime is way more consistent. If a single-lane jams, you stop one small section, fix it in 2 to 3 minutes, and keep going. No other lanes waiting, no whole production line grinding to a halt. For that same snack client, when we went back to them, we didn’t swap their multi-lane—we added a second single-lane machine next to their first. Two single-lanes running 60 pouches per minute each gave them the same total output as the 4-lane (240 per minute), but their uptime jumped back to 90%+, and their changeover time went down too. Why? Changing the pouch size or switch the product? For a single-lane, that’s 10 minutes of swapping a few parts. For a multi-lane? You have to adjust every single lane, which takes 40 minutes minimum, and if you mess up one lane’s settings, all 4 are off.
But wait—don’t get me wrong, multi-lane isn’t useless. There’s a sweet spot where it actually works way better than single-lane. Let’s say you’re a coffee roaster pumping out 200k+ small ground coffee pouches a week, same product, same pouch size, no plans to change that for a year or two. That’s when multi-lane shines. Because you’re not switching products every week, so the long changeover time becomes a non-issue. And with consistent, high-volume output where downtime on a single lane isn’t a regular thing? Multi-lane’s higher pouch-per-square-foot footprint (way less floor space for the same output) pays off. That same coffee roaster I mentioned? They ran a 6-lane machine for 2 years with zero issues, because their setup never changed. But then they launched a cold brew pouch line, and suddenly their multi-lane’s clunky changeover became a bottleneck again. They had to add a single-lane for the new product, because switching the multi-lane from coffee to cold brew would have taken 3 hours—enough to miss their delivery window.
Another big factor people overlook: product compatibility. Single-lane machines are way more flexible for weird or finicky products. If you’re packing something that clumps, or is super light, or has special sealing requirements (like food that needs modified atmosphere packaging, or pharmaceuticals that need airtight seals), single-lane lets you tune each part of the process more precisely. With multi-lane, every lane has to be identical—so if one lane’s seal is slightly off because of product variation, all lanes are off, and you’re wasting product. I had a detergent client a while back who was packing liquid pods. Their multi-lane machine kept leaking because the liquid pods were slightly different sizes, so the sealing jaws on one lane would compress too much or too little. They ended up switching to two single-lane machines, because they could adjust each lane’s sealing pressure independently, cutting waste by 12% almost overnight.
Cost is another thing that’s not just “upfront price.” A multi-lane machine might be cheaper upfront per pouch capacity, but the hidden costs add up fast: spare parts for 4 lanes vs 1, extra maintenance on all those moving parts, higher labor costs because operators have to monitor every lane, not just one. Single-lane has lower upfront per machine, and if you need more output later, adding another single-lane is way cheaper than upgrading or fixing a broken multi-lane. I’ve had clients tell me multi-lane was $50k less upfront, but after two years, they’d spent $30k on repair parts and lost $100k in missed orders from downtime—total cost was way higher than if they’d stuck with single-lane.
Let’s wrap this up with the actual takeaway that most engineers and managers miss: there’s no universal “better” one—it’s all about your production’s specific needs. If you’re just ramping up to 50k to 150k pouches a week, planning to change products or pouch sizes regularly, or packing finicky products that need precise adjustments? Single-lane is almost always the better, more reliable pick. If you’re already cranking out 200k+ pouches a week, never changing your setup, and have floor space to spare? Multi-lane can save you real estate and consistent output.
But here’s the thing: most high-volume production lines that are growing? They’ll outgrow one type before too long. That’s why I always recommend pairing both, instead of choosing one. Have a multi-lane for your steady, high-volume core product, and a single-lane (or two) for new products, small runs, or when you need flexibility without shutting down your whole line.
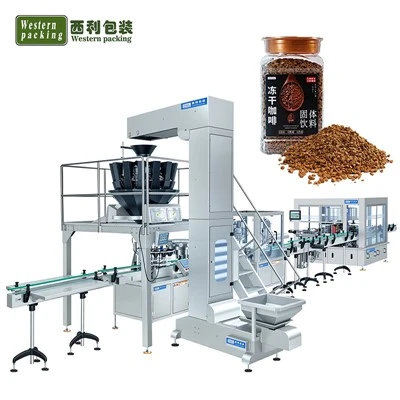
If you’re currently stressing about which one will actually keep up with your volume targets without costing you a fortune in downtime or wasted product, I’m here to help. I can walk you through your actual weekly output, changeover schedule, and product type to figure out what makes sense for your line, no sales pitch, no hard sell—just real advice from someone who’s been in your shoes more times than I can count.
Granule Packaging Machine REFERENCES
- "VFFS Machine Selection: Key Factors for High-Volume Production", Packaging Technology and Science, 2022
- "Downtime Optimization in Continuous Packaging Lines", Journal of Industrial Packaging, 2021
- "Flexibility vs. Throughput: Balancing Production Needs for Small to Mid-Sized Manufacturers", Manufacturing Engineer Quarterly, 2023
- "Product Compatibility in Vertical Form Fill Seal Systems", Food Packaging & Shelf Life, 2020
Guangzhou Western Packing Co., Limited
Guangzhou Western Packing Co., Limited is one of the most professional vertical form fill seal machine(VFFS) manufacturers and suppliers in China, also supports custom service. With abundant experience, we warmly welcome you to wholesale durable vertical form fill seal machine(VFFS) at competitive price from our factory.
Address: No.3, Yilong street, Wulonggang, Zhongluotan Twon, Baiyun District, Guangzhou
E-mail: david@westernpacking.com
WebSite: https://www.westernpackingusa.com/
